Soldadura manual
What Shielding Gas for TIG Welding?
1 de septiembre de 2022
How to choose the right shielding gas for TIG welding? Is there a gas suitable for any material that can be TIG welded?
Antti Kahri
Argon and Helium are the most common shielding gases for TIG welding
The term TIG (tungsten inert gas) welding implies that shielding gas for TIG welding must be inert, and can’t contain any active components. As such, two different gases, argon (Ar) and helium (He), can be used as main gas components. The most common shielding gas for TIG welding is pure argon because it is suitable for any type of material that can be TIG welded. Pure argon provides a stable and narrow welding arc, excellent arc ignition, and relatively low heat input and penetration. These characteristics make pure argon suitable for most TIG welding applications and typically, it is the only shielding gas that hobby welders and professional welders need.
A mixture of argon and helium with 30, 50, or 70% helium is used when welding requires high heat input. Pure helium can even be used when a particularly high heat input is required, for example, when welding thick copper material. Helium also makes the penetration profile wider and deeper. As such, a mixture of argon and helium, or even pure helium, is suited for efficient welding with greater penetration. However, arc ignition characteristics with helium are not as good as with argon and this should be taken into consideration when choosing TIG welding devices. When using pure helium, a powerful high-frequency spark and adjustable ignition parameters are very beneficial.
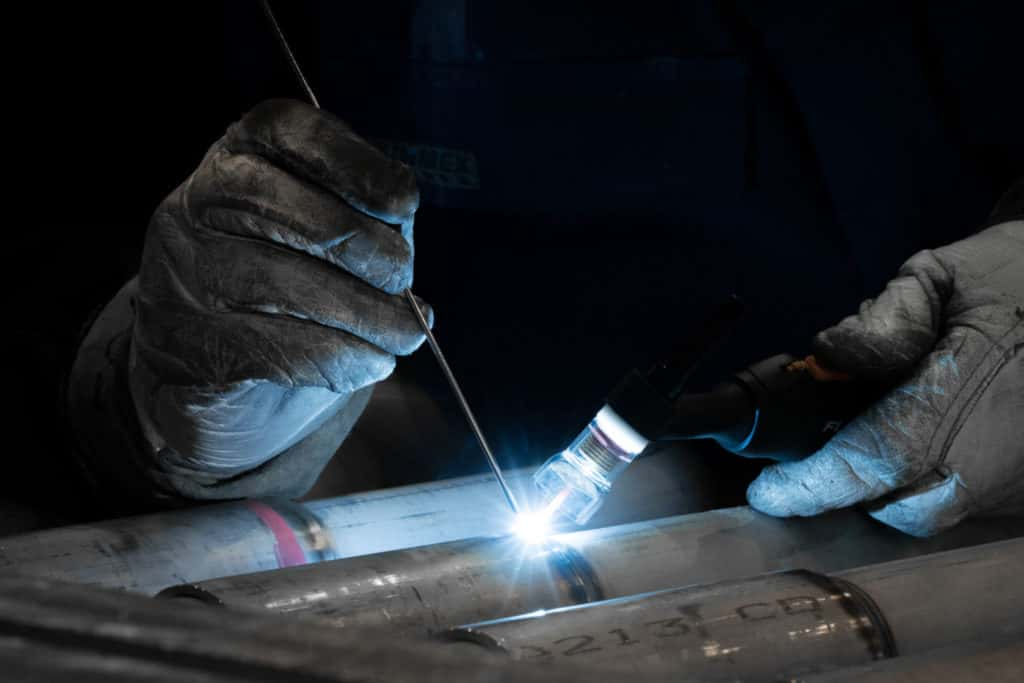
TIG welding
TIG welding can contain a mixture of argon and additive gases; hydrogen, nitrogen and nitrogen oxide
In addition to these two main components, shielding gases for TIG welding can contain:
hydrogen (H2)
nitrogen (N2)
nitrogen oxide (NO)
A small amount of hydrogen (for example 2-6 %) can be used to improve weld pool fluidity for increased penetration or a reduction reaction. In practice, when welding austenitic stainless steels, brighter weld colors can be achieved when hydrogen is used in the shielding gas. However, hydrogen must not be used with ferritic or ferritic-austenitic steels because of hydrogen embrittlement.
When welding high-alloyed austenitic steels or super-duplex steels, a nitrogen loss reaction is quite common. When using filler wire, this reaction is taken into account by using wire with the ideal chemical composition. TIG welding of high-alloyed steels can also be done without filler wire and nitrogen loss can be compensated for by using a small amount of nitrogen (approx. 1.8 %) in the shielding gas. The purpose of nitrogen oxide is to improve the working environment by removing ozone. In some cases, it can also improve arc stability. The typical amount of nitrogen oxide is quite small, (e.g. 0.03 %).
The quality of shielding gas flow matters
A shielding gas flow has a significant effect on weld quality. A highly turbulent flow offers poor shielding and elevated gas consumption while a smooth laminar gas flow provides excellent weld pool shielding and economic gas usage.
A highly turbulent shielding gas flow with a market standard gas lens versus a smooth laminar gas flow with Kemppi gas lens kit.
Read more about Kemppi consumables and get to know >>> the Flexlite TX TIG torch range.
Antti Kahri
Antti Kahri
A respected expert in the field of welding, who tragically passed away in early June 2025 while pursuing his passion on a fly fishing trip. As a Welding Engineer on Kemppi Oy’s Welding Team, he held the prestigious International Welding Engineer (IWE) qualification and brought over a decade of experience to developing advanced welding characteristics for TIG, MIG/MAG, and MMA welding machines, including the renowned X8 MIG Welder and MasterTig. Known for his deep expertise and commitment to welding excellence, he was passionate about enhancing the quality and efficiency of welding through user-friendly innovations. His legacy lives on in the technology he helped shape and in the inspiration he offered to colleagues and the wider welding community.
Productos relacionados
Familia de productos
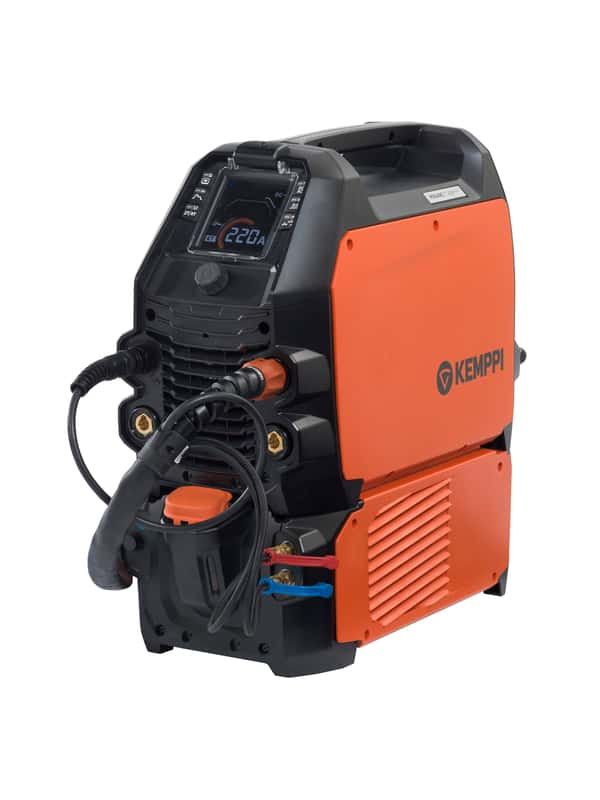
Minarc T es una máquina de soldadura portátil multivoltaje que le permite realizar soldaduras TIG CA/CC de alta calidad y una limpieza profesional de la soldadura con una sola máquina.
Familia de productos
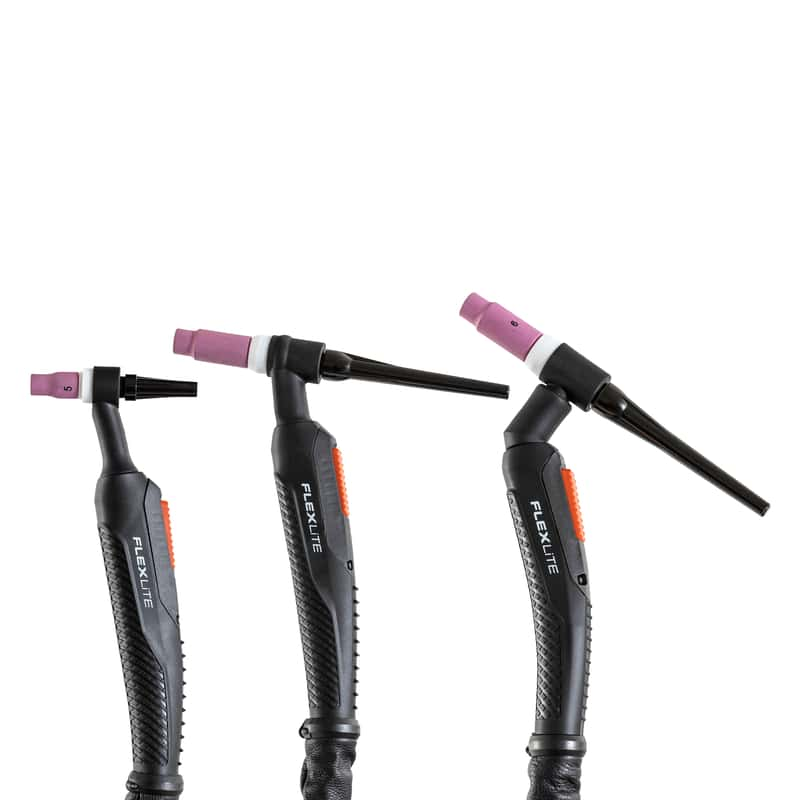
Las pistolas de soldadura Flexlite TX están diseñadas para su uso con equipos de soldadura TIG de Kemppi. La gama de pistolas incluye varios modelos de cuello, lo que redunda en un excelente rendimiento de refrigeración y buen acceso a diseños de juntas difíciles.
Más publicaciones del blog
Behind the scenes - designing the new MasterTig
In welding equipment, creating a good and innovative design goes far beneath the surface. The equipment must be practical, functional, ergonomic, safe, reliable and cost-effective – while still maintaining an aesthetic appeal. Kemppi’s designers and engineers have applied user-centered design philosophy to numerous welding machines introduced since the company’s founding over 70 years ago – and most recently in the creation of the new generation MasterTig with complementary Flexlite TX TIG welding torches.
Innovación
The secret of a good user experience
What are the factors behind a good user experience? The recipe for the world’s best welding experiences has been developed in Kemppi R&D for over 70 years. Jussi Kapanen, Kemppi’s User Experience Manager, now reveals the ingredients.
Innovación
Find the right parameters for TIG welding
Successful welding relies upon a combination of parameter settings and choices.
Fundamentos de soldadura
How Laser Welding Could Reshape Fabrication by 2035
Laser welding is already changing how fast manufacturers can work. Its bigger potential lies in what happens around the weld. From scarce skills and faster changeovers to earlier quality control and better use of production capacity, we look at how laser could reshape fabrication by 2035.
Soldadura manual, Innovación
What 10,000 Welds Reveal About Laser Welding Productivity
What is the real cost of a weld? Kemppi's comparison of laser, MAG and TIG welding goes beyond welding speed to examine the factors that shape production costs, from labour hours and consumables to heat input, finishing and rework. Discover how seemingly small differences can add up across thousands of welds, freeing production capacity, improving efficiency and strengthening the business case for laser welding.
Innovación, Soldadura manual
How Rapid Welding and Kemppi Built a Partnership That Lasts
Rapid Welding has worked with Kemppi since the company opened in 1990. Co-founder and Managing Director Roy Edwards highlighted the principles behind that 36-year partnership, from choosing the right welding solution and supporting equipment throughout its life to addressing the skills shortage and finding the right place for automation and laser welding.
Automatización de la soldadura, Soldadura manual, Fundamentos de soldadura