Svetsning ABC
How to weld aluminum
7 maj 2024
Some metals, like aluminum, have a naturally occurring, tough surface oxide layer. That surface oxide layer must be removed to enable successful welding. In the case of aluminum alloys, the surface oxide layer has a significantly higher melting temperature (approximately 2000°C) than the melting temperature of the aluminum base material (660°C).
Antti Kahri
With TIG (Tungsten Inert Gas) welding, the tough surface oxide is typically broken down and dispersed using alternating current (AC). This is because DC- welding (Direct Current, negative polarity), which has good penetration characteristics, doesn’t provide enough heat to remove the oxide layer, and it doesn’t have a cleaning effect on the weld pool like DC+ welding (Direct Current, positive polarity) does. On the other hand, DC+ delivers too much heat to the electrode and causes it to melt, which is not wanted in TIG welding. Unlike aluminum, for example, carbon steels, stainless steels, copper, and titanium can be welded using DC-.
AC TIG welding
During the AC TIG welding process (Figure 1), the arc burns between a tungsten electrode and the workpiece, protected from atmospheric contamination by an inert gas shield (typically, the shielding gas used is commercial-grade pure Argon). As the welding arc ignites and burns, the high temperature of the tungsten electrode ionizes the argon atoms within the argon shielding gas column. The resulting reciprocating, negatively charged electrons, and positively charged ions, together with the AC (alternating positive and negative half-cycle current waveform), break down the aluminum surface oxide, establishing a controlled welding process that has an optimal balance of cleaning effect, heat input, and penetration.
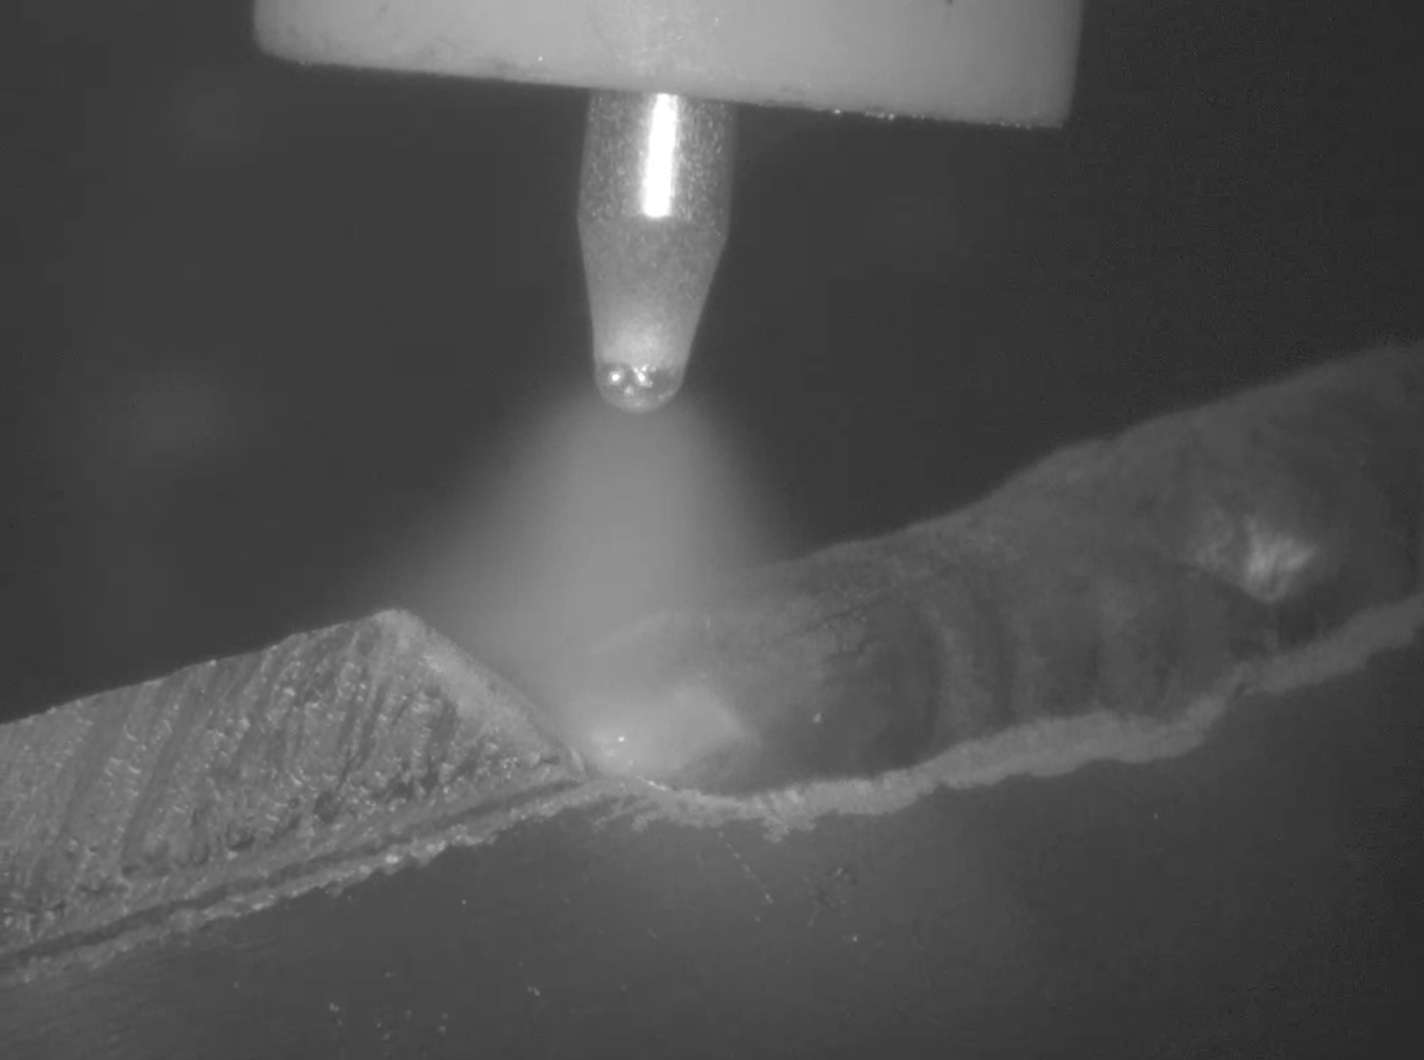
Figure 1. AC TIG welding of the aluminum corner joint. This figure shows the DC- phase of the process that gives the weld its penetration.
Pulsed MIG welding
In MIG (Metal Inert Gas) welding, the wire electrode is melted so DC+ can be utilized. This means that there is enough heat in every typical MIG welding process to remove the aluminum oxide layer. To ensure the best possible welding quality, like in AC TIG welding, the oxide layer and weld pool should be dispersed while welding. In MIG welding, this can be done most efficiently by using a pulsed current (pulsed MIG welding, Figure 2). The variation of welding current helps to keep the process stable and to achieve high-quality, clean welds that are free from porosity. This effect can be taken even further by using stepping movement while welding or by using double pulse welding. In double-pulse welding, the wire feed speed is also pulsed, and this increases the stirring effect in the weld pool.
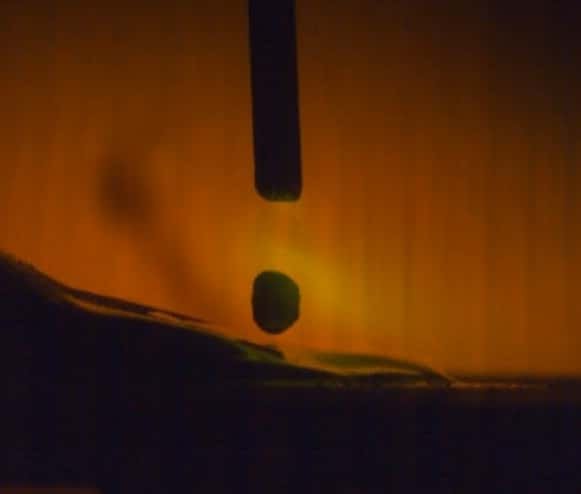
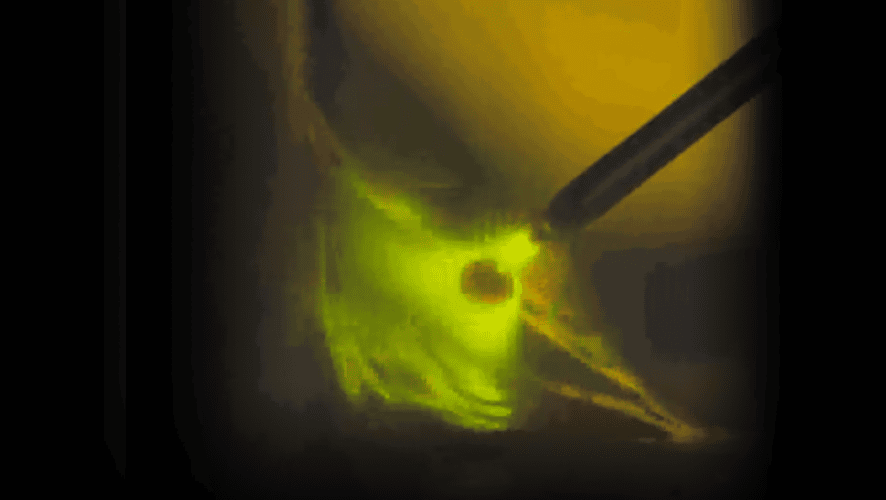
Figure 2. Pulsed MIG welding detaching a droplet from 1,2 mm AlMg5 filler wire.
The best portable welding machines for Aluminum
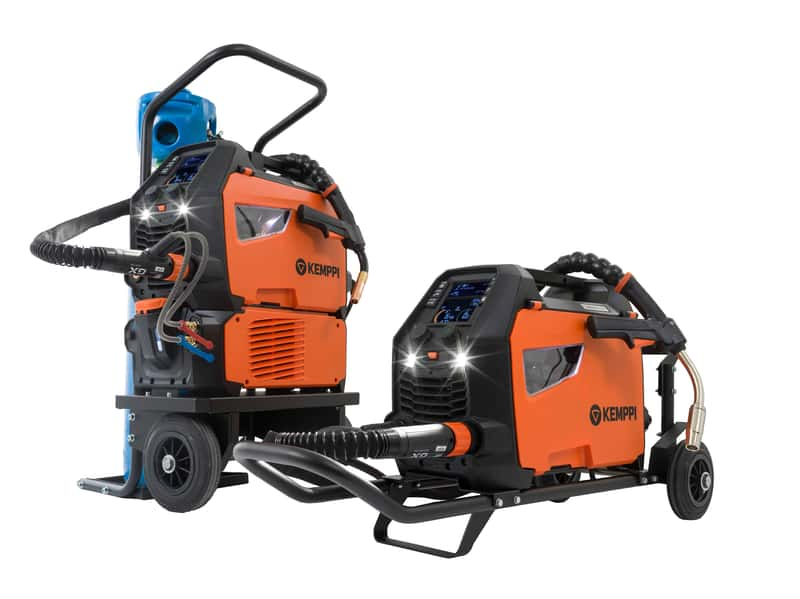
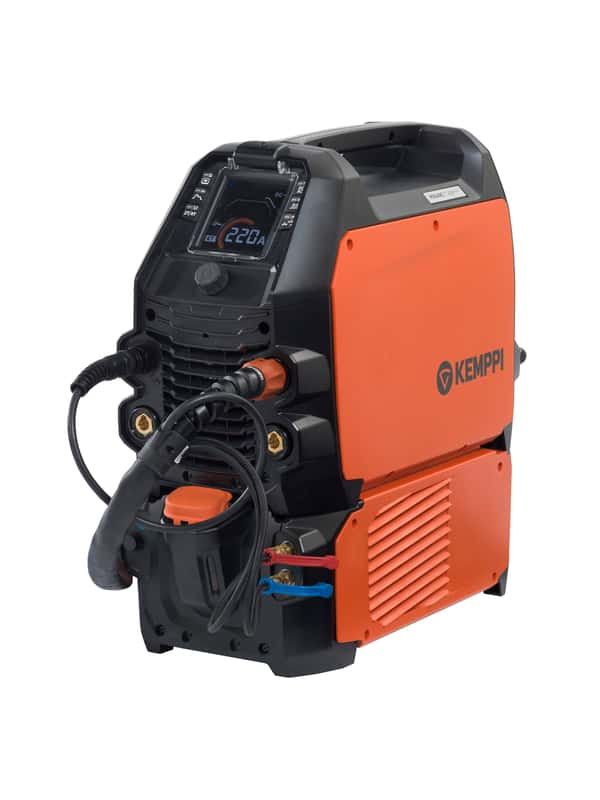
A good TIG welding solution for aluminum is the Minarc T 223 ACDC. It’s an entirely new 220 A, 1-phase, multi-voltage 220V-240V / 110V-120V, AC/DC TIG, and MMA welding machine that includes an electrolytic weld cleaning process as standard. Now, in seconds, you can weld and electrolytically clean your perfect welds with one machine. Another portable welding machine that is perfect for aluminum MIG welding is the Master M 205. It stands out from most of the other 1-phase MIG welding machines because it offers a professional-level pulse welding process.
Antti Kahri
Antti Kahri
A respected expert in the field of welding, who tragically passed away in early June 2025 while pursuing his passion on a fly fishing trip. As a Welding Engineer on Kemppi Oy’s Welding Team, he held the prestigious International Welding Engineer (IWE) qualification and brought over a decade of experience to developing advanced welding characteristics for TIG, MIG/MAG, and MMA welding machines, including the renowned X8 MIG Welder and MasterTig. Known for his deep expertise and commitment to welding excellence, he was passionate about enhancing the quality and efficiency of welding through user-friendly innovations. His legacy lives on in the technology he helped shape and in the inspiration he offered to colleagues and the wider welding community.
Relaterade produkter
Produktfamilj
Master M 205 och Master M 323 sätter en ny standard för kraft och prestanda i en bärbar MIG/MAG-svetsmaskin. Tack vare sin kompakta, lätta konstruktion som är lätt att bära får du en bärbar MIG/MAG-svetsmaskin som du kan ta med dig vart du än behöver den.
Produktfamilj
Minarc T är en bärbar svetsmaskin som gör att du kan utföra högkvalitativ AC/DC TIG-svetsning och professionell svetsrengöring med en och samma maskin.
Fler blogginlägg
High-quality pulse welding with a 1-phase MIG/MAG welding machine
The versatility of portable welding equipment has traditionally been limited by the lack of pulsed MIG/MAG welding. It has been argued that three-phase power is required to achieve high-quality MIG/MAG pulse welding.
Manuell svetsning
What is pulsed MIG welding, and for what you can use it?
Pulsed MIG/MAG welding is a significant improvement in welding technology, offering accuracy, productivity, and flexibility that conventional welding methods can hardly compete with. This advanced process has become popular for professionals looking to improve weld quality, especially in demanding applications. Here's a closer look at how pulsed MIG/MAG welding works and the situations where it truly shines.
Svetsning ABC
What to consider when buying a welding machine?
Once a welding machine has reached the end of its life cycle, or a company expands its operations, it's time to find a new best friend for the welder. There is a wide range of welding machines on the market, and in many cases, comparing different brands and models is challenging. What kind of things should be considered when purchasing a welding machine?
Svetsning ABC
How Rapid Welding and Kemppi Built a Partnership That Lasts
Rapid Welding has worked with Kemppi since the company opened in 1990. Co-founder and Managing Director Roy Edwards highlighted the principles behind that 36-year partnership, from choosing the right welding solution and supporting equipment throughout its life to addressing the skills shortage and finding the right place for automation and laser welding.
Automatisering av svetsning, Manuell svetsning, Svetsning ABC
Säkerhet som anpassas efter svetsarens utmaningar och varierande risker
Svetssäkerheten ställer allt större krav. Riskerna vid ljusbågen är desamma, men moderna arbetsförhållanden innebär att exponering kan lagras under längre arbetspass och i begränsade inomhusutrymmen. Följaktligen måste personlig skyddsutrustning för svetsning betraktas både som ett skydd för svetsaren och som ett bevis på att kraven uppfylls. Hos Kemppi utformas och valideras personlig skyddsutrustning för svetsning i praktiken genom tydliga krav, synpunkter från svetsare samt verifierad överensstämmelse med EU:s förordning 2016/425 om personlig skyddsutrustning, CE-märkningsprocesser och relevanta EN-standarder.
Säkerhet, Svetsning ABC
Eurosatory 2026 And the Future of Defence Manufacturing
Eurosatory 2026 highlighted a clear shift in modern defence manufacturing. While defence systems are becoming more digital, networked, and autonomous, their foundation remains physical. From armoured vehicles and artillery to industrial resilience, welding quality, steel structures, and production discipline remain paramount to defence readiness.
Digitalisering, Innovation