Welding ABC
Choosing the right gas nozzle length for MIG (GMAW) welding
7 November 2023
Gas nozzle length is an important feature in a MIG welding torch because nozzle length has an effect in contact tip heat load, contact tip spatter protection and welding current.
Visa-Valtteri Monto
If the distance between the contact tip and work piece is too short, the contact tip is prone to failure because of extreme radiation heat from the weld puddle and welding arc. The contact tip and gas nozzle are also prone to spatter sticking to them due to high heat, and spatter sticking to the contact tip hole can cause contact tip burnback. In general, if the contact tip to workpiece distance is too short, pulse welding processes might not work correctly.
A longer nozzle will extend the contact tip to workpiece distance, which leads to a decrease in welding current (most MIG welding processes are constant voltage processes, and therefore the power source will keep the voltage constant as the current is allowed to change). The reduction of welding current is greater if the welding wire has lots of electrical resistance, as is the case with stainless steel wires. On the other hand, aluminum and its alloys have low electrical resistance, and therefore electrode extension length has little effect in welding current.
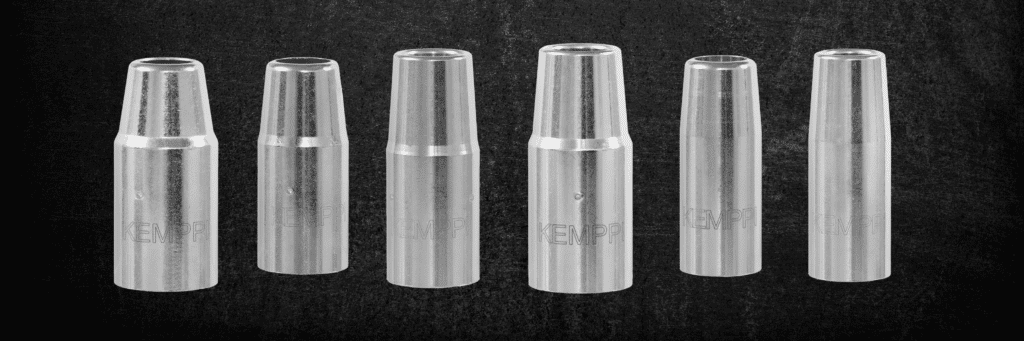
Kemppi offers three gas nozzle lengths and you can choose the model that best suits your application. The short gas nozzle model extends 1.5 mm over the end of the contact tip, the medium nozzle extends 3.5 mm over the contact tip, and the long model has 5.5 mm of extension. The medium nozzle model comes as standard equipment on our torches.
Aluminum welding
Aluminum and its alloys have low electrical resistance and therefore extending the contact tip to workpiece distance does not decrease welding current significantly. Kemppi recommends using the long gas nozzle model for all aluminum welding applications to protect the contact tip from radiative heat and welding spatter.
Ferritic steel welding
Ferritic steel welding wires (also known as mild steels or structural steels) have more electrical resistance than aluminum wires, but not as much as stainless steel wires. When welding thin plates with thin wires, it is recommended to use the short gas nozzle or the medium nozzle model, depending on preference, to ensure good weld puddle control as contact tip to workpiece distance can be kept short and welding current is high.
For medium-power and all-round applications, the middle-length gas nozzle serves as a balancing point between spatter protection and heat protection for the contact tip. A long nozzle is recommended for high-power applications and flux core wire welding. The long nozzle model can also be beneficial in tack welding if the welder prefers to tack by pushing the gas nozzle to the plates in fillet welding. Flux cored wires require the stick out length to be long enough to pre-heat the wire to evaporate any moisture in the core and burn away any lubricants used in wire manufacturing.
Stainless steel welding
Stainless steel wires have high electrical resistance, which causes the welding current to decrease sharply when contact tip to work piece distance is increased. In low- to medium-power applications, a contact tip distance that is too long causes the weld puddle to not flow correctly, which compromises the weld bead appearance and weld penetration. The short gas nozzle model is recommended for most stainless steel welding for better weld puddle control. In high-power stainless steel welding, the medium gas nozzle model can be beneficial, as it provides better spatter and heat protection for the contact tip.
Visa-Valtteri Monto
Visa-Valtteri Monto
Welding Engineer, Kemppi Torches & Aftermarket. International Welding Engineer (IWE), who has experience in developing welding characteristics of GMAW welding machines and GMAW welding torches. Has been working with welding torch development and troubleshooting since 2019. Interested in helping out customers thrive by making Kemppi products even better.
Related products
Product family
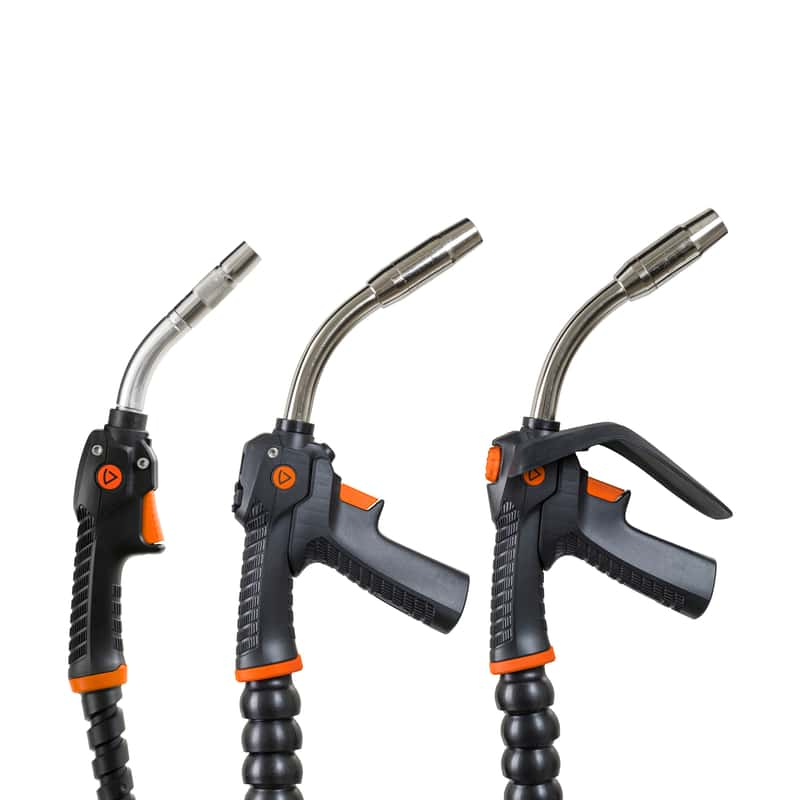
The Flexlite GXe MIG/MAG torch series is built to meet the demands of professional welders who need reliability, precision, and durability in every weld. Designed for demanding welding tasks, the Flexlite GXe enables excellent control, precision, and comfort – day after day, weld after weld.
Product family
Flexlite GX product series contains welding guns to be used in MIG/MAG welding processes. All Flexlite GX welding guns enjoy the Flexlite features for user comfort, welding efficiency and extended consumable parts life. The GX family includes a wide range of welding gun models designed to serve specific welding needs.
More blog posts
The heat resistance of the HD welding gun makes a welder's work more efficient
When the workload gets heavy and the days get longer, both welders and their welding guns heat up. Emotions can be cooled down with a cup of coffee, but the welding gun only cools down by taking regular breaks. To keep these breaks as short as possible, optimizing the thermal conductivity and heat resistance of the welding gun are important in daily work.
Manual welding
MIG/MAG welding arc types
In MIG/MAG welding, the mode of material transfer between the filler wire and the weld pool changes in line with the welding current.
Welding ABC
The best way to eliminate spatters
When it comes to welding gun performance, cooler is definitely better. But is there an optimal temperature for a water-cooled welding gun? And how do you keep the gas nozzle and contact tip spatter-free? Let's find out by answering a few questions.
Welding ABC
How Rapid Welding and Kemppi Built a Partnership That Lasts
Rapid Welding has worked with Kemppi since the company opened in 1990. Co-founder and Managing Director Roy Edwards highlighted the principles behind that 36-year partnership, from choosing the right welding solution and supporting equipment throughout its life to addressing the skills shortage and finding the right place for automation and laser welding.
Welding automation, Manual welding, Welding ABC
Safety that keeps up with welders' challenges and changing risks
Welding safety has become increasingly demanding. The hazards at the arc remain constant, but modern working conditions mean exposure can accumulate over longer shifts and in tighter indoor spaces. As a result, welding PPE needs to be treated as both protection for the welder and proof of compliance. At Kemppi, welding safety PPE is designed and validated in practice through clear requirements, welder-led feedback, and verified compliance with EU PPE Regulation 2016/425, CE marking processes, and relevant EN standards.
Safety, Welding ABC
Eurosatory 2026 And the Future of Defence Manufacturing
Eurosatory 2026 highlighted a clear shift in modern defence manufacturing. While defence systems are becoming more digital, networked, and autonomous, their foundation remains physical. From armoured vehicles and artillery to industrial resilience, welding quality, steel structures, and production discipline remain paramount to defence readiness.
Digitalization, Innovation