Innovatie
Wat 10.000 lassen onthullen over de productiviteit van laserlassen
28 oktober 2026
Wat kost een las écht? Aan de hand van Kemppi's vergelijking van laser-, MAG- en TIG-lassen kijken we verder dan lassnelheid: naar lasuren, beschermgas, toevoegmateriaal, warmte-inbreng en nabewerking. Ontdek hoe kleine verschillen bij grote productievolumes optellen en invloed kunnen hebben op capaciteit, productiviteit en rendement.
Varsha Saraogi
Onderwerpen:
In science fiction, lightsabers help save the galaxy. In the real world, saving 20 seconds can make or break an empire.
Twenty seconds sounds almost meaningless. Until it happens 10,000 times. Then it becomes more than 55 hours of production time, almost seven eight-hour shifts that could potentially be spent finishing another batch, reducing a backlog or starting the next customer project.
Welding speed gets attention because it is easy to measure. Start the stopwatch. Make the weld. Stop the clock. But the customer is not paying for welding speed. They are paying for finished parts. And that changes the calculation.
At a time when manufacturers are already struggling to add skilled welding capacity, it’s increasingly imperative to improve production productivity from the hours you already have. The European Labour Authority's report places welders and flame cutters among Europe's top shortage occupations.
A Kemppi technical comparison of laser, MAG and TIG welding gives us a useful way to look at what that could mean.
What did Kemppi compare?
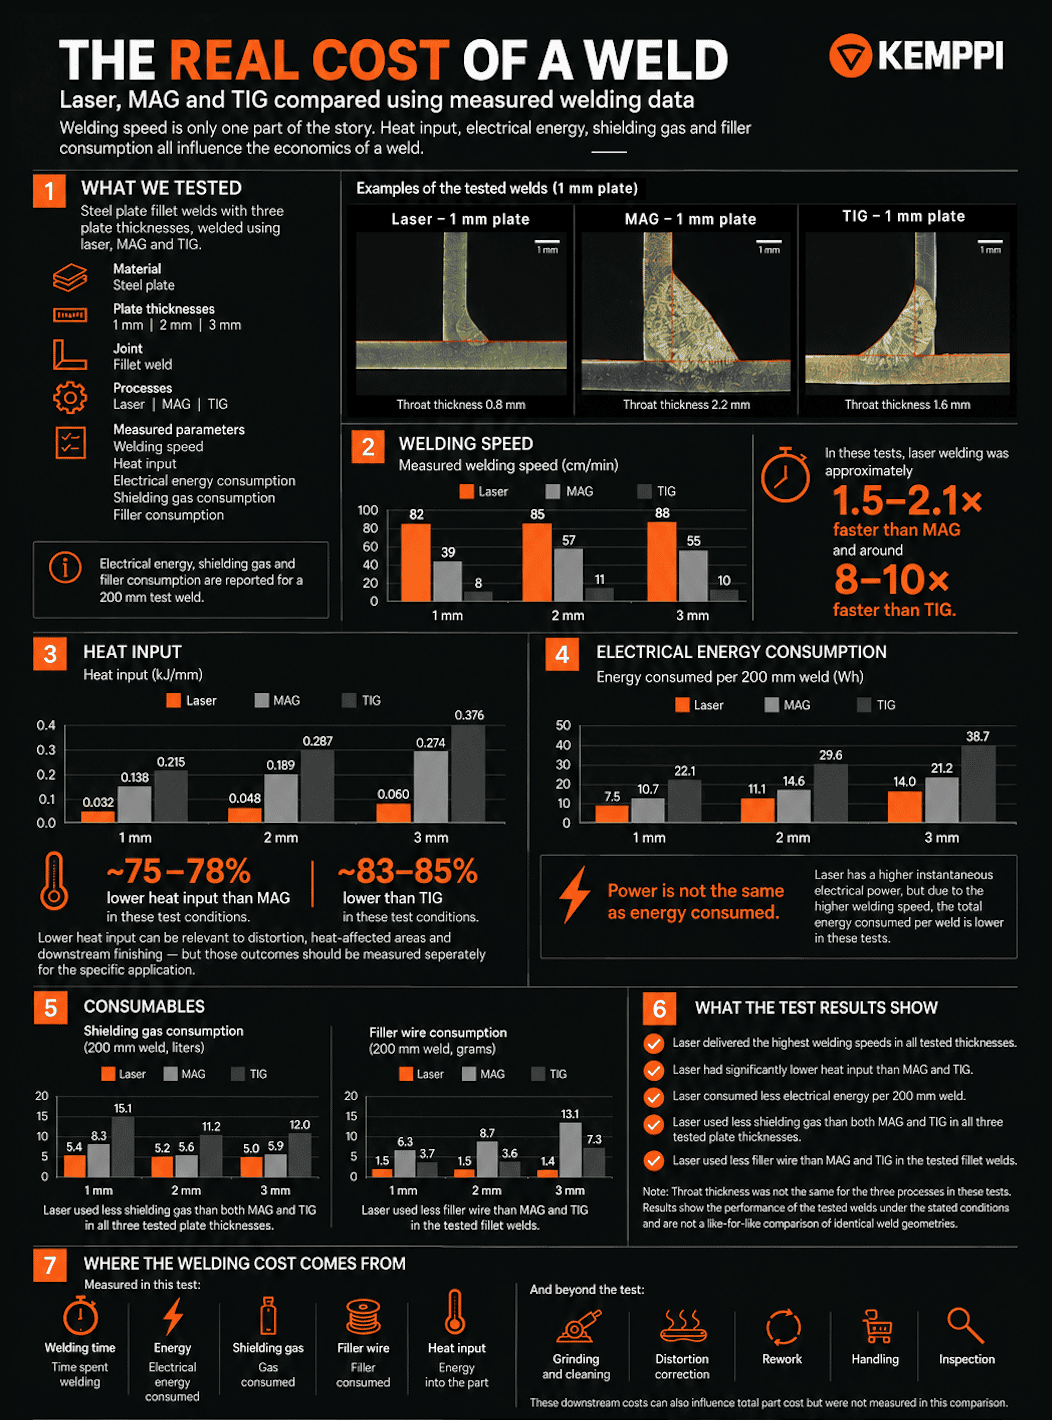
We compared laser, MAG and TIG fillet welds on 1, 2 and 3 mm steel plate.
The tests measured:
welding speed
heat input
electrical energy consumption
shielding gas consumption
filler consumption
For energy, shielding gas and filler, the results are based on a 200 mm test weld.
The comparison does not mean the three processes are interchangeable. In particular, the resulting throat thicknesses differed between the tested welds, which is important when interpreting consumable use and other results.
What the data does reveal is how dramatically the resource and time profile of a weld can change with the process. And that is where the business case begins.
How much production time can welding speed actually release?
Across the three plate thicknesses, measured welding speeds were:
Plate thickness | Laser | MAG | TIG |
|---|---|---|---|
1 mm | 82 cm/min | 39 cm/min | 8 cm/min |
2 mm | 85 cm/min | 57 cm/min | 11 cm/min |
3 mm | 88 cm/min | 55 cm/min | 10 cm/min |
Under these test conditions, laser welding was approximately 1.5–2.1 times faster than MAG and around 8–10 times faster than TIG.
Let's scale just one of the tests. For the 2 mm steel test, the exact measured speeds were 851 mm/min for laser, 571 mm/min for MAG and 107 mm/min for TIG.
If a manufacturer had 10,000 welds of 200 mm each, those speeds translate approximately into:
Process | Welding time for 10,000 × 200 mm welds | Equivalent 8-hour welding shifts |
|---|---|---|
Laser | 39 hours | 4.9 shifts |
MAG | 58 hours | 7.3 shifts |
TIG | 312 hours | 39 shifts |
That means the measured laser speed would represent approximately 19 welding hours of released capacity compared with MAG in this example.
Against TIG, the difference is approximately 272 welding hours.
Note that this is a welding-time extrapolation from one controlled test, not a prediction of total production time or guaranteed FastBeam³ savings. Preparation, positioning, fit-up, safety procedures, inspection and other operations are not included, and the tested weld geometries differed.
But it illustrates an important point. A few seconds per weld can add up to entire production shifts at scale. The business value of those hours depends on what you do with them.
For instance, 19 hours could become another production batch, creating capacity for another customer project. Or it could allow experienced welders to spend more time on joints and applications that genuinely require their expertise.
Where does laser welding fit in?
If welding is the bottleneck, business growth can therefore depend on questions such as:
How many components can each available welding hour produce?
Which welds genuinely require the highest level of manual skill?
Can repetitive or suitable applications be completed differently so skilled welders can focus elsewhere?
Laser welding does not eliminate the need for welding expertise. Process selection, joint design, material knowledge, quality control and safe operation remain critical. But in suitable applications, increasing output per welding hour can help manufacturers address the capacity problem from another direction. What happens when one minute disappears from every part? If a process improvement removes just one minute from every component, the annual capacity released becomes:
Annual production | One minute saved per part |
|---|---|
1,000 parts | 16.7 hours |
5,000 parts | 83 hours |
10,000 parts | 167 hours |
50,000 parts | 833 hours |
100,000 parts | 1,667 hours |
At 100,000 parts, it is more than 200 eight-hour production shifts.
And after the welding stops?
Welding speed is only one place where production time can disappear.
Another is rework.
Low heat input is normally discussed as a technical welding characteristic. For the business case, however, the more interesting question is what lower heat input can mean downstream.
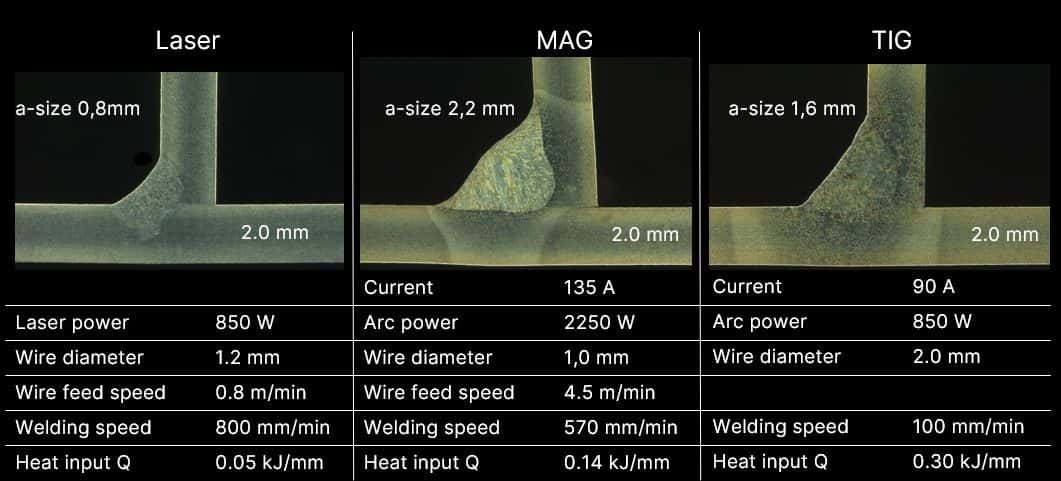
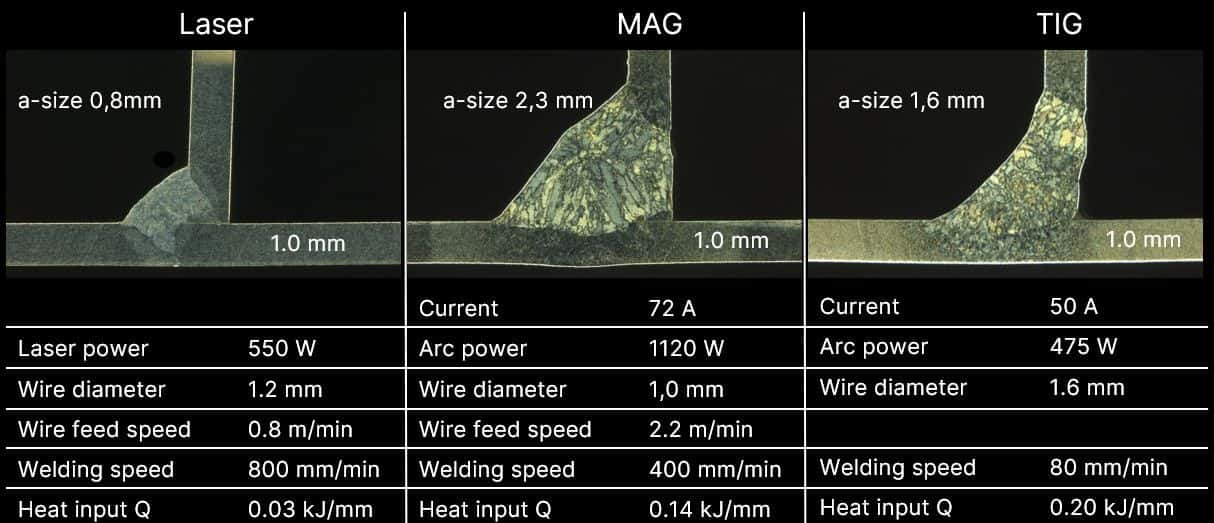
In Kemppi's tests, laser heat input was substantially below MAG and TIG across all three tested plate thicknesses. For example, on the 2 mm plate it measured:
Laser — 0.048 kJ/mm
MAG — 0.189 kJ/mm
TIG — 0.287 kJ/mm
That makes heat input interesting because lower thermal input can help reduce distortion in suitable applications.
And distortion has a very real labour cost. TWI research into European shipbuilding reported that rework associated with inaccuracies and thermal distortion had been estimated at 15–30% of labour costs for new ship construction in some applications. TWI identified reduced distortion and reduced straightening and rework as one of the important economic motivations for laser and laser-hybrid welding in shipbuilding.
Removing work after welding can sometimes create more value than making the weld itself faster.
That is also why current laser-manufacturing research increasingly looks beyond raw process speed. Fraunhofer ILT describes industrial laser-production challenges in terms of shorter cycle times, lower scrap, reduced energy consumption, better material utilisation, process stability and reliable quality - all of which determine whether a high-speed process actually delivers value in series production.
What happens to consumables when production scales?
Then there are costs that seem small because they disappear a few grams or litres at a time.
Based on Kemppi's 2 mm steel plate test, with a weld length of 200 mm:
Consumable | Laser | MAG | TIG |
|---|---|---|---|
Shielding gas per weld | 5.2 L | 5.6 L | 11.2 L |
Shielding gas for 10,000 welds | 52,000 L | 56,000 L | 112,000 L |
Filler material per weld | 1.5 g | 8.7 g | 3.6 g |
Filler material for 10,000 welds | 15 kg | 87 kg | 36 kg |
Again, this should not be interpreted as a universal percentage saving because the weld throat thicknesses were different. In the 2 mm test, the recorded throat thicknesses were 0.8 mm for laser, 2.2 mm for MAG and 1.6 mm for TIG. This is exactly why production-specific ROI matters.
Once a manufacturer enters its real wire price, gas price and annual weld volume, grams and litres become extra expenditure.
The ROI of laser welding
For a manufacturer considering FastBeam³, the useful ROI equation needs more than welding speed. It should consider:
Production volume: How many relevant parts or metres of weld are produced annually?
Welding hours: How much operator time does the existing process require?
Preparation and fit-up: Does the application provide the joint consistency required by the process?
Finishing: How much grinding, cleaning or cosmetic work follows welding?
Distortion correction How much labour is spent bringing welded parts back into tolerance?
Rework and scrap: How often does work have to be corrected or discarded?
Consumables: How much filler, gas and other consumable material does each process require?
Energy: What is the actual energy consumption per completed part?
Investment: What equipment, training, maintenance and laser-safety infrastructure are required? What is a released production hour worth to your business?
Saving those same 100 hours in a workshop with a six-week backlog can allow the business to accept more orders without immediately adding another shift or welding station.
That is where welding productivity can become commercial capacity.
Three workshops. Three different laser welding business cases.
Imagine three manufacturers considering the same technology.
The high-volume subcontractor
It makes thousands of similar sheet-metal assemblies with stable fit-up.
Five or ten seconds repeated thousands of times matters. Faster welding, reduced consumable use and shorter downstream processing can combine into meaningful annual capacity.
Its biggest opportunity may be throughput.
The stainless-steel fabricator
Volumes are lower, but visible weld quality matters. Significant labour goes into grinding, cleaning and correcting distortion.
Its largest saving may not come from welding speed at all.
It could come from reducing everything that happens after welding.
The high-mix workshop
It produces constantly changing components, small batches and joints with varying fit-up.
Laser speed may look impressive in a demonstration, but the shop may not be able to exploit it on every job. MAG and TIG can remain the better choice for many applications.
Its challenge is therefore finding the right laser applications, rather than replacing every existing process.
Laser does not replace MAG or TIG
A useful question is: Which parts of our production would create more value if we welded them differently?
Kemppi's tests show that, under the tested conditions, laser delivered higher welding speeds, lower electrical energy consumption per 200 mm test weld, lower gas consumption and lower filler consumption than the corresponding tested MAG and TIG welds.
Those figures do not tell every manufacturer to make the same decision.
Instead, look at the welding seconds. Then multiply them by annual volume.
Look at the finishing minutes, rework, the welding hours currently limiting production.
Look at what another 20, 100 or 500 available hours could mean to the order book.
Because the strongest business case is what your company can do with the time it gets back.
Gerelateerde producten
Productfamilie
FastBeam 3 is een in Finland geproduceerd 3 kW handheld fiberlaser lasapparaat voor snel en gecontroleerd lassen van staal, roestvast staal en aluminium. Integratie van Penetration Shape Control en Weld Assist maken nauwkeurige procesaanpassing, snellere instelling en digitale traceerbaarheid mogelijk bij industrieel laserlassen.
Meer blogberichten
How does steel welding benefit from special processes?
Welding mild steels may often be considered a simple task. However, welding these steels has specific characteristics that can make the welding process challenging.
Handmatig lassen, ABC van het lassen
Kemppi's advanced welding processes: MIG/MAG welding
One of the most important elements in developing welding equipment has long been improving welding processes and creating new process variations. Modern measurement and arc control methods have made a wide range of variations in the arc welding process possible. These advanced welding processes significantly improve welding production efficiency and weld quality. This article presents the special processes and operations developed by Kemppi for MIG/MAG welding.
ABC van het lassen, Handmatig lassen
How Rapid Welding and Kemppi Built a Partnership That Lasts
Rapid Welding has worked with Kemppi since the company opened in 1990. Co-founder and Managing Director Roy Edwards highlighted the principles behind that 36-year partnership, from choosing the right welding solution and supporting equipment throughout its life to addressing the skills shortage and finding the right place for automation and laser welding.
Lasautomatisering, Handmatig lassen, ABC van het lassen
Safety that keeps up with welders' challenges and changing risks
Welding safety has become increasingly demanding. The hazards at the arc remain constant, but modern working conditions mean exposure can accumulate over longer shifts and in tighter indoor spaces. As a result, welding PPE needs to be treated as both protection for the welder and proof of compliance. At Kemppi, welding safety PPE is designed and validated in practice through clear requirements, welder-led feedback, and verified compliance with EU PPE Regulation 2016/425, CE marking processes, and relevant EN standards.
Veiligheid, ABC van het lassen
Eurosatory 2026 And the Future of Defence Manufacturing
Eurosatory 2026 highlighted a clear shift in modern defence manufacturing. While defence systems are becoming more digital, networked, and autonomous, their foundation remains physical. From armoured vehicles and artillery to industrial resilience, welding quality, steel structures, and production discipline remain paramount to defence readiness.
Digitalisering, Innovatie
How AI Supports Quality, Traceability, and Flexibility in Robotic Welding
The AITOOLS1 webinar explored how AI-assisted process control, machine vision, synchronized data, and machine learning models are advancing robotic welding automation, improving quality management, traceability, and production flexibility for demanding industrial production.
Lasautomatisering, Innovatie, Digitalisering